01 The Fundamental Objective of Rational Subgrouping
Rational subgrouping is the cornerstone of Shewhart control charts. The main purpose of rational subgrouping is to collect measurements in such a way that variation within a subgroup represents only short-term, natural process noise (common causes). Meanwhile, any operational shifts or disturbances occurring over time are allowed to manifest between subgroups.
If within-subgroup variation includes extraneous factors—such as mixing parts from different shifts, multiple machine spindles, or distinct raw material batches—the estimated process variation becomes inflated. As a result, control limits expand beyond their true width, concealing real process shifts and rendering the control chart insensitive to emerging issues.
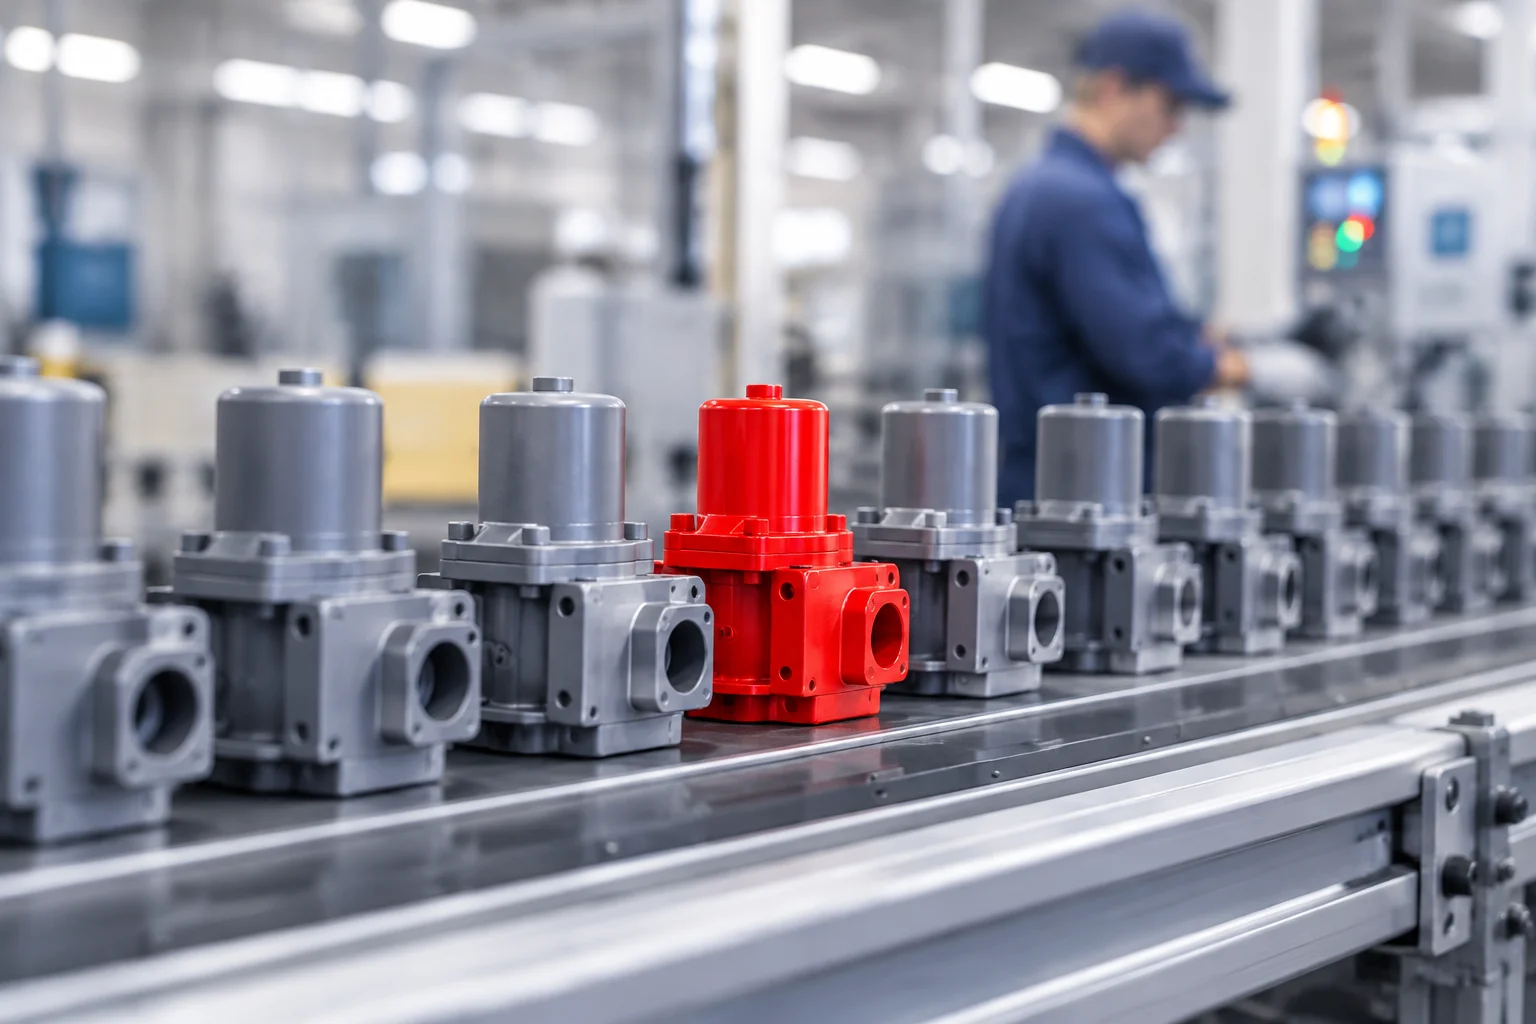
An ideal subgroup is structured so that items within the group are produced under conditions as identical as possible, allowing true operational changes over time to stand out clearly.
Process Engineering Review
Discuss your statistical variation observations with an atlas specialist.
02 Key Strategies for Structuring Rational Subgroups
Selecting an effective subgrouping scheme depends heavily on the physical process and the specific failure modes under investigation. Quality engineers generally utilize three distinct sampling strategies:
- Instantaneous Sampling: Selecting consecutive items produced at virtually the same point in time. This minimizes variation inside the subgroup and maximizes sensitivity to process shifts occurring between sample intervals.
- Periodic Representative Sampling: Taking individual measurements at set intervals throughout a shift. While this can capture gradual intra-shift drift, it requires caution to ensure internal variation does not artificially stretch control limits.
- Stream Isolation: Keeping data from separate nozzles, cavities, or operators in distinct subgroups rather than combining them into a single blended subgroup.
03 Avoiding Common Subgrouping Errors
One of the most common pitfalls in statistical process analysis is combining measurements from multiple parallel sources into one subgroup. For instance, averaging outputs from four parallel production lines into a single subgroup masks line-to-line differences, treating real structural variation as unexplainable noise.
Another mistake is choosing excessively large subgroup sizes. While larger subgroups increase sensitivity to minor mean shifts, they also increase the probability of capturing special causes within the subgroup itself. Maintaining small subgroups (typically 4 or 5 consecutive units) preserves diagnostic clarity and keeps control limits mathematically sound.
Optimize Your Process Subgrouping Strategy
Consult with our statistical specialists to review your sampling frequency and control chart limit calculations.
Contact Our Engineering TeamFrequently Asked Questions
A subgroup is rational when all units within it are gathered under virtually identical process conditions. This ensures that only natural common-cause variation exists inside the subgroup, enabling control limits to clearly reveal process changes between subgroups.
A subgroup size of 4 or 5 provides an optimal balance: it offers sufficient statistical sensitivity to detect meaningful mean shifts while keeping the sampling window short enough to prevent special causes from corrupting the within-subgroup variation.
If special causes or mixed process streams contaminate the within-subgroup data, the calculated range or standard deviation becomes artificially high. This causes the control limits to be too wide, blinding the control chart to actual shifts in process performance.